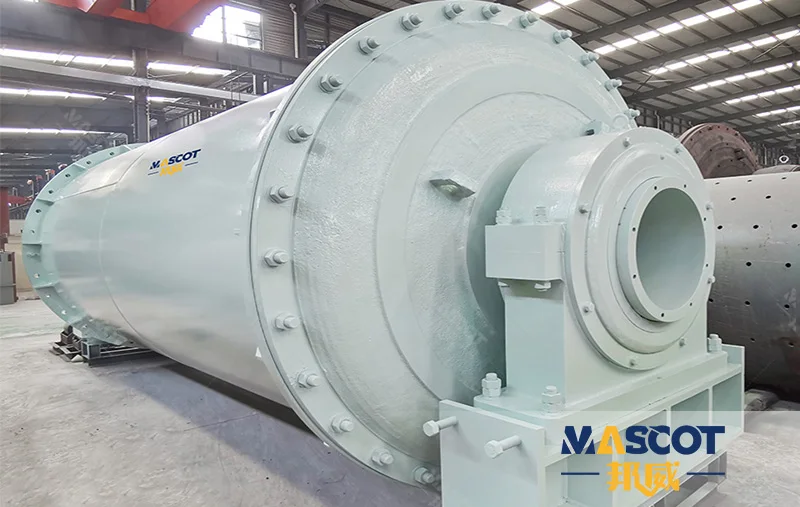
In glaze and feldspar preparation the mill is not judged on how hard it grinds but on how consistently it grinds the same recipe twice. That consistency is built almost entirely in the slurry: how much solid is in it, how freely it moves, how long the media has to work on it and how the whole charge behaves inside the cylinder. Get those right and a ceramic mill delivers the same slip, batch after batch, with no iron anywhere in the product. Get them wrong and the plant ends up re-tuning every lot by feel. Using the published specification of the Ceramic Ball Mill, this article sets out what batch and continuous operation actually change about slurry control, and which of the two a plant should specify.
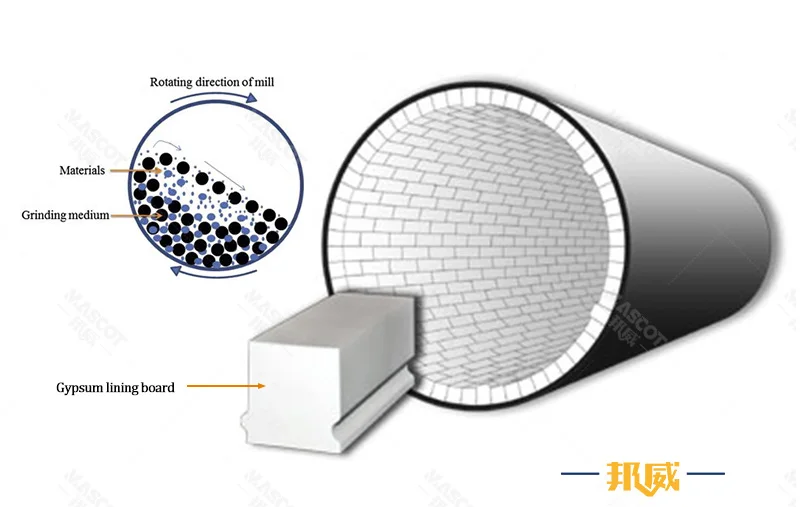
A ceramic mill is a sealed cylinder lined with high-alumina ceramics and charged with alumina media, rotating at 65-80% of critical speed. Inside that cylinder the media do two different jobs at once: the cascading portion fractures particles by impact, while the sliding portion refines them by attrition. Fineness is adjustable from 100 microns down to sub-micron by tuning residence time and media size, which is the reason one machine can serve several grades for several customers.
Four parameters decide how well that happens, and all four are held to the recipe rather than adjusted by ear:
| Parameter | What It Controls | What Goes Wrong When It Is Off |
|---|---|---|
| Grinding time | How much surface the charge develops before the product is released | Too short and the target residue is never reached; too long and the plant burns energy producing fines it cannot sell |
| Media size | Whether the charge breaks particles by impact or refines them by attrition | A media charge that is too coarse reaches the residue target slowly and wears the lining harder while it tries |
| Solid concentration | How the slurry moves, and how the media interact with it | A thick slip cushions the media and cuts grinding efficiency; a dilute slip raises wear per ton and lengthens the drying stage downstream |
| Rotation speed | The motion pattern inside the cylinder — cascade, cataract and slide | Outside the working band the grinding action does not form properly, and the charge neither lifts nor rolls as intended |
Notice that two of the four parameters are properties of the slurry rather than of the machine. That is why slurry control, not mill selection, is usually the difference between a plant that holds its recipe and one that does not.
Solid concentration does two jobs at once, and only one of them is about grinding. Inside the mill, the density of the slip sets how freely the media can move and how efficiently the fines are carried away from the grinding zone. A slip that is too thick cushions the charge: the media spend their energy pushing through a viscous mass instead of striking particles, the batch takes longer, and the extra time is paid for in both power and lining wear. A slip that is too thin swings the problem the other way — less cushioning, more metal-free but more ceramic-on-ceramic and media-on-lining abrasion per ton of product, plus a larger volume of water that has to be removed later.
Outside the mill, that water is a cost. In wet grinding the process fluid becomes part of the product: the same slip that grinds well in the cylinder has to be dewatered, dried or spray-dried further down the line, and every extra litre entering the circuit is energy spent removing it. This is the part of slurry control that does not appear on a mill datasheet but does appear on the plant's electricity bill.
Practically, solid concentration is a recipe decision rather than an operating preference. It should be fixed against the material and the downstream process, before the mill is ordered, and then held. A plant that adjusts solids to chase a residue target is using the wrong lever: residence time and media size are what change fineness, and solids is what changes how efficiently the charge works while doing it.

Glaze preparation is normally run as a batch operation, and the reason is commercial rather than mechanical. A glaze is a recipe — frit, feldspar, clay and water in fixed proportions — and what the customer buys is a colour and a fired surface that must match the last delivery. Running that recipe as a discrete batch means the whole lot is ground together and discharged together, so there is no question about which material ended up in which shipment.
Batch mode also makes quality verification possible at the point of production. The lot can be tested for residue and iron content before it leaves the grinding bay, and if it is off-specification it is rejected before it becomes somebody's rejected container rather than after. The reference installation in Section 7 works exactly this way, at a stable 2.8 tons per batch.
The discipline batch operation demands is that the four parameters are held to the recipe rather than tuned by feel. A batch cycle is only repeatable if grinding time, media size, solid concentration and rotation speed are set the same way every time — which is the practical argument for a mill that allows all four to be set precisely instead of approximated.

Body preparation and mineral powder production are usually run continuously at steady throughput, because there the constraint is tonnage rather than lot identity. In continuous operation the mill is never reset: material flows in and out, and the control target shifts from “did this batch reach specification” to “is the circuit holding steady”.
That shift matters more than it first appears. Without a discharge-and-replace step, the top cut of the product is fixed by the discharge and classifier configuration rather than by the operator's judgement at the end of a cycle. Any drift on the feed side — a change in moisture, a change in slurry density, a slower or faster feed — travels straight through to the finished powder, because there is no batch boundary to stop it. The instrumentation and the feed control therefore carry more of the quality burden in continuous mode than they do in batch mode.
| Aspect | Batch Mode | Continuous Mode |
|---|---|---|
| Feed | A weighed recipe charged as one lot, fed wet as slurry | A steady feed, wet as slurry or dry as powder |
| Control target | The four recipe parameters are held for the cycle, then the lot is discharged and replaced | Steady state is held; control moves to feed rate, slurry density and the discharge configuration |
| Where it fits | Glaze preparation and colour-critical, small-lot work where the whole lot must be identical | Body preparation and mineral powder production where tonnage, not lot identity, is the constraint |
| How fineness is set | By residence time, media size, solids and rotation speed within the cycle | By residence time in the cylinder and the discharge or classifier setting |
| Main risk to watch | Batch-to-batch variation if the recipe is tuned by feel instead of held | Feed-side density or moisture drift, which passes straight into the product |
| Iron contact | Zero — provided the contact zone is ceramic throughout | Zero — provided the contact zone is ceramic throughout |
The most useful thing about the ceramic series for a plant that makes more than one product is that the machine does not have to be chosen between the two modes. It is configurable for wet or dry operation without hardware changes, by adjusting the feed method: wet grinding feeds material as a slurry, dry grinding feeds powder with optional ventilation. This is why ceramic tile and sanitary ware factories often run a single model line for both glaze preparation (wet) and body preparation (dry).
The decision belongs at order stage rather than in the plant, because the discharge arrangement is configured to match the intended operating mode. If a mill is going to be asked to do both jobs, say so before the order is placed and the configuration will be specified for it.

A wet circuit is more forgiving of particle size and less forgiving of contamination than a dry one, because a slip carries anything it has picked up straight into the batch. That is why the material-contact zone has to be ceramic through the whole path — cylinder lining, end covers, discharge grate and grinding media — and not just at the point that is easiest to line.
The standard specification is a 92% high-alumina lining, with 95% ultra-high alumina offered for the most demanding purity or wear conditions; the liners have a compressive strength exceeding 850 MPa and are precision-cut to interlock inside a steel shell that absorbs impact. The ceramic does the contact work, the steel does the structural work, and under normal operating conditions with materials below Mohs 7 the alumina lining lasts 3-5 years — against 1-2 years for rubber and 12-18 months for manganese steel in abrasive service. A material composition certificate is issued with every shipment, which is what turns a purity claim into a checkable fact.
Slurry control and liner choice are the same argument seen from two directions. A steel-lined mill in a wet glaze circuit is not simply a contamination risk on paper: typical iron pickup runs at 0.05-0.15%, against below 0.008% on a fully ceramic contact zone — and for a product judged on fired colour, that difference is a rejection rate rather than a specification.
A Vietnamese producer needed 325-mesh silica powder for the solar glass industry — a market where the iron specification is tight enough that a batch failing it is scrap. The problem was upstream of the customer's quality laboratory: an existing steel ball mill was leaching iron into the powder, the batch rejection rate had reached roughly 12%, and solar glass manufacturers were threatening to switch suppliers. A single rejected container represented a $18,000-$35,000 loss in product value before freight was added.
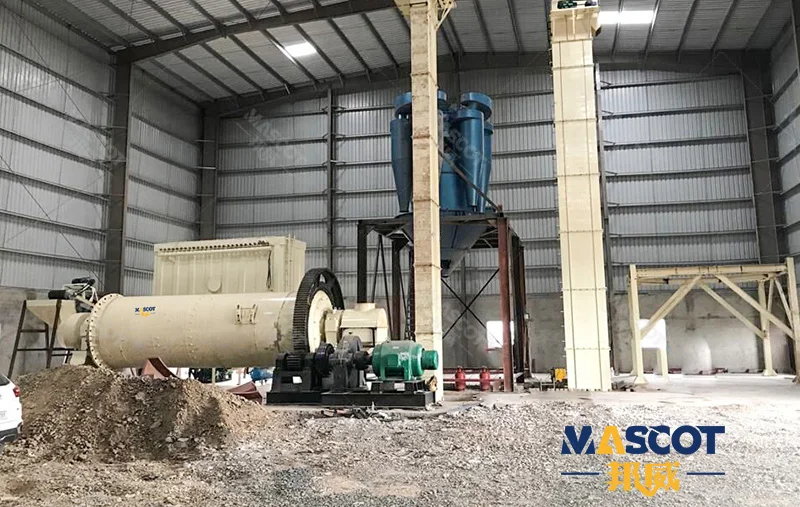
The solution was an MCBM-1830 ceramic ball mill configured with a 92% high-alumina lining and alumina grinding balls, with the full material path — cylinder, end covers, grate and media — running ceramic. Iron content in the finished powder stabilised below 0.008%, acceptable at certified international solar-glass grade. The batch rejection rate fell from roughly 12% to below 1%, the mill settled into a stable output of 2.8 tons per batch that matched the production schedule, and annual maintenance spend came down by 40% with the lining still in service after three years.
Read as a slurry-control case rather than a hardware case, the lesson is that the mill was specified around the recipe: the batch size, the solids and the target residue were settled first, and the machine, the media and the lining were then configured to hold them.
Q1: Should I run my ceramic mill in batch or continuous mode?
A: It follows the product, not the preference. Glaze preparation is normally batched, because the customer is buying an identical lot and the lot has to be verifiable before it ships. Body preparation and mineral powder production are normally continuous, because there the constraint is tonnage. One machine can serve both patterns; the discharge configuration is what has to match the mode, and it is confirmed at order stage.
Q2: What is the single most important slurry variable?
A: Solid concentration, because it changes grinding efficiency, wear per ton and the downstream drying load at the same time. A slip that is too thick cushions the media and slows the batch; a slip that is too thin raises abrasion per ton and adds water that later has to be removed. Fix it against the material and the downstream process, then hold it.
Q3: Can one mill grind both wet and dry?
A: Yes. The ceramic series is configurable for either mode without hardware changes — wet grinding feeds material as a slurry, dry grinding feeds powder with optional ventilation. Only the feed method changes and the discharge is configured accordingly. Confirm the intended mode, or modes, at order stage.
Q4: What fineness and speed does the mill work at?
A: Discharge fineness is adjustable from 100 microns down to sub-micron by tuning residence time and media size, with the cylinder rotating at 65-80% of critical speed. The working point is set by grinding time, media size, solid concentration and rotation speed, which is why those four values belong in the recipe as fixed numbers rather than as operator judgement.
Q5: How do I know the lining will not contaminate the slip?
A: By asking which internal parts are ceramic and what documentation comes with the unit. A mill with an alumina cylinder lining but a steel discharge grate is not an iron-free mill, however good the lining is. The Mascot specification runs ceramic through cylinder lining, end covers, discharge grate and media, with a material composition certificate issued for each shipment, and the reference installation holds iron below 0.008% against a typical 0.05-0.15% for a steel-lined circuit.
Slurry control is what separates a ceramic mill that repeats a recipe from one that has to be re-tuned for every lot. Four parameters do the work — grinding time, media size, solid concentration and rotation speed — and two of them are properties of the slip rather than the machine, which is why they have to be settled before the mill is ordered rather than discovered during commissioning. Batch operation suits glaze, where the lot has to be identical and verifiable; continuous operation suits body preparation and mineral powder, where the constraint is tonnage and the quality burden shifts to feed control and the discharge configuration.
The Ceramic Ball Mill covers both patterns in one machine and in either wet or dry service, with an alumina contact zone rated at 3-5 years under Mohs 7 materials and iron pickup below 0.008%. Where a plant also prepares dry body mixes or mineral powders at coarser fineness, a Dry Ball Mill complements the ceramic unit in the same flow sheet; where the product has to go beyond 325 mesh into the ultra-fine range, the HGM Series Micro-powder Grinding Mill takes over. Send your material, target residue, batch size or required tonnage, and the lining grade, media charge and cycle can be specified around your recipe.

About of Mascot
Zhengzhou Mascot Industry is a high-tech mining equipment company integrating R&D, manufacturing, sales, and after-sales service. Focusing on crushing, grinding, and mineral processing equipment, we provide professional solutions to our customers. We are ISO9001:2015 certified, and our products include mobile crushing plants, crawler crushing plant, construction waste crushing plants, jaw crushers, sand making machines, cone crushers, fine crushers, grinding mills, ball mills, etc., all with reliable performance to meet diverse project needs.
• Professional pre-sales support: Free project design and comprehensive solutions to help you accurately select the right equipment;
• Comprehensive on-site service: Providing installation guidance and worker training to ensure smooth equipment commissioning;
• Reliable after-sales guarantee: A complete after-sales system, timely response to technical inquiries and equipment maintenance, ensuring long-term stable operation.
To protect your rights, please contact us through the following official channels for professional service:
WhatsApp: 0086-16650273865
Email: mascot@mascotenv.com
We are committed to providing high-quality equipment and full-cycle services to deliver comprehensive intelligent solutions for the global mining industry!

YGMX Enhanced High-Pressure Mill is a new type of high-performance grinding equipment, and the biggest improvement of this milling equipment lies in the increase of the high-pressure spring system in the grinding roller part. Compared with the traditional high-pressure roller mill, it has a wider scope of application and excellent performance to meet the production needs of a variety of powder fineness. It is widely used in non-metallic minerals, chemicals, building materials, metallurgy, environmental protection, etc. Multiple areas.
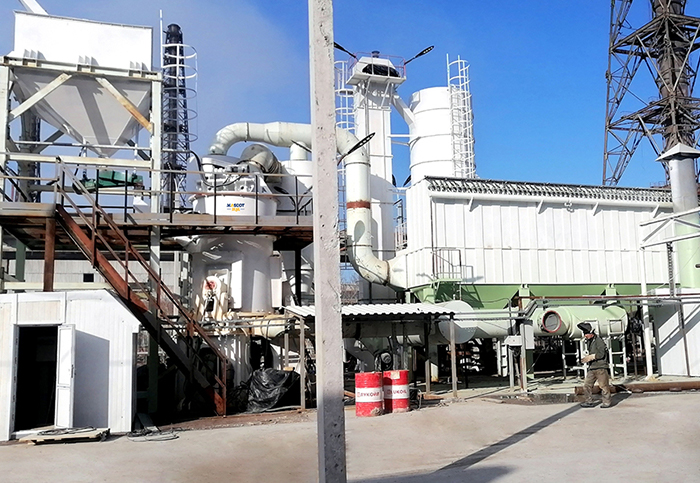
The production line of the vertical roller mill is a cost-effective and energy-efficient solution for processing powder, which is widely used in many industries, such as metallurgy, building materials, industrial solid waste treatment, thermal power plants, cement plants, and environmental protection fields. The primary purpose of this project is to finely grind raw materials through a vertical roller mill to meet the requirements of different industries for particle size, purity, and output of powder products.

This production line utilizes a three-ring medium-speed micro-grinding mill as the central equipment, complemented by other auxiliary equipment like hammer crushers, bucket elevators, and storage silos to establish a comprehensive grinding operation system. It has demonstrated strong potential for application and market competitiveness in industries such as construction, chemical industry, and new materials.

The Raymond mill production line is a highly efficient system designed for grinding operations, with a focus on energy efficiency, durability, and productivity. It caters to the needs of users by offering fine powder products in non-metallic ores, coal powder, and slag processing, aiding enterprises in achieving sustainable growth.

The high-pressure grinding mill production line is a project specially designed for efficient grinding operations. It is widely used in metallurgy, building materials, the chemical industry, highways, water conservancy hydropower, and other industries. It is a suspended roller mill that uses springs to increase pressure. It can achieve efficient grinding processing of various non-metallic raw materials. It has high efficiency, stability, and environmental protection characteristics.
Green and Intelligent Mining Machinery
Manufacturing and Export Base
Based on high quality and perfect after-sales service, our products have been
exported to more than 120 countries and regions.
Copyright © 2023 Zhengzhou Mascot Environmental Technology Co., Ltd Record number: Yu ICP No. 13021523-4




 WhatsApp
