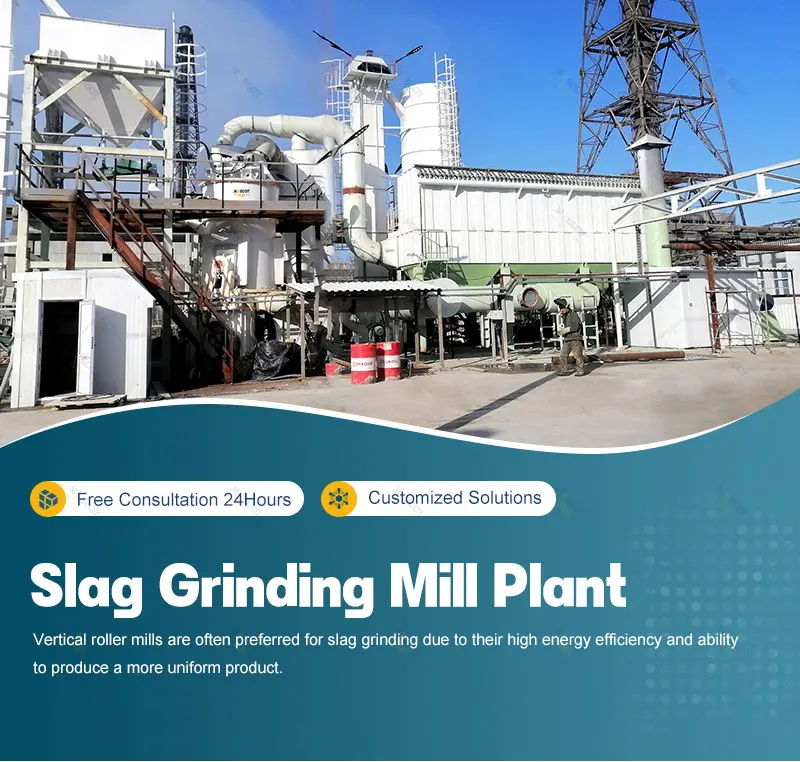
Two complaints dominate the calls that come from a running Vertical Roller Mill: the mill is shaking, or the rejects have gone up. They arrive together often enough that plants treat them as one fault, which is the first mistake, because they are measured in different places and corrected in different places. Vibration is a mechanical signal from the grinding bed and the hydraulics beneath it. Rejects — depending on which reject the operator is counting — are either a protection device doing its job or a classification circuit telling you that the feed has changed. This guide separates the two, sets out the causes behind each, and gives the checking order that finds the answer without stopping the plant for a day.
A vertical roller mill grinds by compression in a material bed. Material is fed to the centre of the rotating grinding table, centrifugal force carries it outward under hydraulically pressurised rollers, and it is crushed layer by layer between the rollers and the table — the arrangement described in the series' own working principle, where metal-to-metal contact is avoided and wear on abrasive material stays low.
Every element of that description is a vibration variable. The bed has to be continuous and of consistent depth, the material has to arrive at the centre of the table rather than at its edge, the rollers have to carry the pressure the bed was designed for, and the hydraulic system has to hold that pressure as the components wear. Disturb any of those and the mill shakes: the grinding bed loses its uniformity and the rollers begin to ride on it unevenly.
Rejects are a different chain. On this mill family there are two devices that discharge material and one that returns it, and they are not the same thing:
A rising figure from the first device is a feed-quality message. A rising figure from the second is a tuning or wear message. Treating them as one number is how a plant ends up adjusting the classifier to compensate for scrap iron in the feed.

Start every investigation by deciding which of the four numbers is actually moving. They are measured in different places, and only two of them indicate a problem with the mill.
| Which Reject | What It Is | What a Rise Means | What to Do |
|---|---|---|---|
| Reject gate discharge | Automatic discharge of hard, ungrindable material that would damage the rollers | The feed is carrying more foreign material — typically scrap metal in slag or steel slag, or oversize tramp from the quarry | Work upstream: the discharge is protective and the mill is behaving correctly; check the scrap handling and pre-crushing stage |
| Classifier coarse return | Oversize particles returned to the table for regrinding; the circulating load | Either the target fineness has been moved or the bed has changed; this is a tuning signal, not a fault | Confirm the target mesh, then check feed rate, bed behaviour and wear parts before touching the classifier speed |
| Separator coarse discharge | Cyclone stage sending particles above roughly 50 µm back for regrinding in a closed circuit | Classification efficiency has fallen — usually through adhesion, agglomeration or a fouled separation zone | Check feed moisture and the separator internals; on wet or humid feed the separation zone needs its anti-adhesion protection to be intact |
| Finished-powder rejects (QC) | Product failing the residue or pass-rate specification at the laboratory | The mill's output no longer matches the specification the plant is selling | Sample at steady state and check the two usual causes: wear parts out of profile, and an unsteady feed |
How to read this table: the four rows describe how rejects are counted and handled on this mill family. The devices and their behaviour are the published description of the series; the third column states what a rising figure means in practice. Note the design intent behind the first row: an automatic reject gate is a feature that converts a potential breakdown into a routine discharge, so a moderately higher discharge rate with steady mill behaviour is not a fault to be tuned out.
The single most important sentence in the series' operating description is that stable, centred feeding is what keeps mill vibration low and protects the hydraulic system. Material is fed to the centre of the rotating table so that it spreads into an even bed before the rollers reach it; feed that arrives off-centre produces a bed that is deeper on one side, and a roller riding an uneven bed is what the plant feels as shaking.
The published note adds why this matters more on some duties than others: on slag it matters more than on soft minerals, because the bed is heavier. A heavy, abrasive bed amplifies the same disturbance, which is why water-granulated slag duty rewards a feeding arrangement that can hold a steady rate — a controlled feed from the stockpile, not a system that surges and starves.
The fix is usually upstream of the mill: verify the feeder's calibration and speed control, confirm that the material is actually reaching the centre of the table, and check that variations in the raw stockpile are not being passed straight through as variations in feed rate.

The rollers are loaded hydraulically, and the pressure is an operating variable rather than a fixed setting: the hydraulic pressurisation station supplies adjustable grinding pressure to the rollers, which the manufacturer identifies as critical for controlling grinding efficiency and finished product fineness.
Two design features are worth knowing when a mill starts to shake, because they tell you which faults the machine is already protected against.
The roller-to-table gap is dynamically maintained. The gap between the grinding roller and the table is held and adjusted by the hydraulic control system; as rollers and table liners wear, the hydraulics compensate pressure to keep the material bed thickness consistent, so neither fineness nor throughput should degrade as the wear cycle progresses. If fineness and tonnage both fall away over a wear cycle, the compensation is no longer holding and the hydraulic side needs attention rather than a classifier change.
A mechanical limit device prevents roller-to-liner contact. The published description states that this device prevents direct contact between the roller sleeve and the table liner, eliminating the destructive impact and severe vibration that can occur in mills without the protection. That is useful in two directions: it means normal operation should not produce metal-on-metal shocks, and if the plant is seeing the violent, rhythmic shaking associated with contact, the limit device and the bed conditions under it are the first places to look.
The table speed is part of the same picture. The grinding table's rotation speed is adjustable on this series, which lets the operator optimise the speed-to-wear relationship against material hardness and target fineness — a control worth re-checking whenever the feed material changes, because a speed that suits limestone may not suit a heavier bed.

Vibration that is not explained by feeding or by the bed usually ends up in the two oil systems, and both are specified with instrumentation that makes the check quick.
The lubrication station. A high/low-pressure lubrication station provides circulating lubrication for critical components such as the grinding roller bearing journals, and the automatic thin-oil system is designed to support 24-hour continuous operation without manual lubrication intervention. A thin-oil circulating system that is running correctly removes one of the classic sources of roller-bearing vibration; one that is starved, or circulating degraded oil, produces exactly the symptom operators describe as roughness in the mill.
The hydraulic station. Hydraulic stations on this series include automatic sensors that alert the operator to pressure changes or filter clogs through the touch-screen interface — which means the first diagnostic step is not an inspection but a review of the alarm and trend history. A hydraulic system that cannot hold pressure produces both a weaker bed and a mill that hunts, and both show up as vibration before they show up as lost tonnage.
On abrasive duties, the same systems carry the reason the series is specified for 24/7 operation in high-dust and high-temperature environments with a low maintenance load. The practical check is the one the control system already offers: read the hydraulic pressure trend and the lubrication condition before opening anything.

When the coarse return rises without any change in target fineness, the cause is usually classification efficiency rather than comminution, and the usual first suspect is moisture. Water-granulated slag arrives at the mill at a moisture content anywhere in the published 4-15% band, dried inside the mill in the same pass as grinding to a final powder moisture of ≤1%; feed well above that band should be drained or blended first so that throughput stays steady.
Material that is sticky rather than merely wet creates a second problem in the separation stage. Powder that agglomerates is graded as though it were coarse, so agglomerated fines are returned to the table and ground again — burning power on material that was already fine, while the residue figure stays stubbornly high. The published answer to this is built into the separator: a pre-dispersion stage that breaks up powder agglomerates before grading, so that the separation zone receives uniformly dispersed material, and an anti-adhesion lining for humid duty.
That failure mode has a documented field precedent. A 90 t/h limestone powder line in Malaysia had been running traditional single-rotor separators with low classification efficiency and frequent blockage when processing wet limestone; the replacement unit used a double-rotor separator with anti-adhesion lining and PLC linkage to the mill, and the reported results were grading efficiency up to 89% with separator power consumption cut by 34% and no adhesion under high humidity. The relevant lesson for a troubleshooting procedure is that a separator that is fouling will also drag the mill's circulating load up — so wet-feed problems present as rejects first and as vibration second.
The order matters, because most of these causes present as the same symptom. Work down the table and stop at the first row that matches what the plant is seeing.
| What You See | First Check | What It Rules Out | The Correction |
|---|---|---|---|
| Shaking with a steady feed rate | Hydraulic pressure trend and lubrication condition on the control panel | Feed-side causes; the fault is in the loading system | Restore grinding pressure and oil circulation before touching any setting |
| Shaking that follows the feed | Whether material is reaching the centre of the table at a constant rate | Wear-part and hydraulic causes | Correct feeder calibration and stockpile handling; on heavy slag beds this is the dominant cause |
| Severe, rhythmic impact | The mechanical limit device and the bed under the rollers | Normal operating variability — this is contact, not load fluctuation | Inspect the limit device, the roller sleeves and the table liner profile |
| Coarse return rising, fineness unchanged | Feed moisture against the published 4-15% band, and separator condition | Classifier setting — do not move it yet | Drain or blend over-wet feed; check pre-dispersion and anti-adhesion protection in the separator |
| Reject gate discharge rising | Scrap handling, pre-crushing and the feed source | The mill itself — the gate is a protective device | Work upstream; keep the wear parts on a planned replacement interval |
| Residue drifting up with constant power | Roller sleeve and table liner profile | Classifier tuning and material change | Schedule the modular wear-part change rather than compensating with settings |
How to read this table: the symptoms are the ones reported on this mill family, and the checks are ordered by how quickly each can be made from the control panel or the feeder rather than by opening the mill. The fourth row is the one most often got wrong: a rising coarse return with an unchanged specification is a moisture or separation problem, and moving the classifier speed hides it while making the tonnage worse.
Every row of the diagnostic table above depends on having a normal value to compare against. Six entries are enough to turn vibration and rejects from anecdotes into trends.
| Record | Why It Matters |
|---|---|
| Feed rate and feed moisture | The two variables that decide whether the bed is stable; most vibration reports trace back to one of them |
| Hydraulic pressure and lubrication condition | The panel already displays them; a trend is what distinguishes a control problem from a mechanical one |
| Main motor current | Shows loading changes that the operator cannot see, and separates a heavy bed from a fouled one |
| Reject gate discharge quantity | Turns a protective function into a feed-quality indicator with a trend line |
| Coarse return / circulating load and target residue | The pair that shows whether the separation circuit is still holding the specification |
| Roller and table-liner inspection dates | The interval that explains fineness drift at constant power, planned rather than discovered |
The best test of a vibration and rejects procedure is a mill running on the feed that stresses it most: wet, heavy, abrasive slag that also carries scrap metal. A grinding station on Vietnam's central coast producing S95 ground granulated blast furnace slag for ready-mix concrete plants had been running an ageing dryer plus ball mill circuit, and needed one energy-saving unit able to dry and grind water-granulated slag at 10-18% moisture to S95 fineness (400-500 m²/kg Blaine) at a stable output above 30 t/h.
The installation is an SRM1700 vertical roller mill system with in-mill hot-air drying, high-chrome wear parts and a high-efficiency dynamic classifier, arranged for direct belt feeding from the granulated slag stockpile — a configuration in which the feeding discipline described in section 3 is a design decision rather than an operator preference.
The reported results: wet granulated slag at 14% moisture is dried to 1% inside the mill in the same pass as grinding, with no separate dryer; specific power for S95 powder is about 40% lower than the circuit it replaced, cutting the monthly electricity bill by roughly one third; and the engineer-led installation and commissioning ran over 40 days, including training the local shift operators on S95 fineness settings. The customer's own summary is the one that matters for this article: "The SRM 1700 has run around the clock since start-up and holds our S95 target every shift."

A complete station of this type is a matched set rather than a mill: crusher, vertical roller mill, bucket elevator, vibrating feeder, classifier, cyclone collector, dust collector and blower, as listed in the 40 t/h vertical mill production line case. That list matters for troubleshooting, because the feeding, classifying and dust stages are where the two symptoms in this article are usually created.
The point of the case for a troubleshooting article is not the tonnage. It is that the two hardest input conditions in the whole application — a heavy bed and a wet feed — were handled by feeding control, in-mill drying and the reject system, which is the same set of mechanisms a plant inspects when a mill starts to shake or a reject figure starts to climb. A line that runs continuously for years on that feed is a line whose feed arrangement was specified properly at the start.
Q1: Why does my vertical roller mill vibrate even though nothing has been changed?
A: Check what changed outside the mill first. Stable, centred feeding is what keeps vibration low, and an unsteady or off-centre feed shows up as shaking before it shows up anywhere else — on slag this matters more than on soft minerals because the bed is heavier. Then read the hydraulic pressure and lubrication trends on the panel: the grinding gap is maintained dynamically, and if pressure compensation is not holding, both fineness and tonnage will drift down over the wear cycle.
Q2: What does "high rejects" actually mean on this mill?
A: It depends which reject you are counting. The automatic reject gate discharges hard, ungrindable material to protect the rollers — that is a feature, and a rise means the feed is carrying more scrap or tramp metal. The classifier's coarse return is the circulating load and should be tuned, not eliminated. A separator's coarse discharge points at classification efficiency and usually at feed moisture. Name the number before you act on it.
Q3: Can wet feed cause high coarse returns?
A: Yes, and it is one of the most common causes. Sticky powder agglomerates and is graded as if it were coarse, so fine material is returned and ground again while the residue figure stays high. The series covers a published feed moisture band of 4-15% dried to a final ≤1% in the same pass; feed well above the band should be drained or blended first, and the separator's pre-dispersion and anti-adhesion arrangements are what keep the grading zone clean on humid duty.
Q4: Is there a protection against metal in the feed?
A: Yes. Hard, ungrindable material is discharged automatically instead of being forced through the grinding zone — the step the manufacturer identifies as the one that keeps unexpected breakdowns out of the production plan on slag and steel slag. Wear parts are supplied as modular high-chrome alloy segments so that a worn or damaged piece is replaced on its own.
Q5: How long should the wear parts last?
A: Roller sleeves and table liners are manufactured in high-chromium alloy with a published service life exceeding three years under standard operating conditions, and on limestone duty the mill can run continuously for six months without replacing any wear component. Modular segments and standard stock availability are what make the change a planned stop.
Q6: What service and warranty terms apply?
A: A 12-month warranty covers the whole machine and a further 12-month warranty covers core components such as rollers, table liners and classifiers, with 24/7 online consultation and engineers available for on-site installation, commissioning and operator training. Spare parts are supplied from stock for the service life of the mill.
Vibration and rejects are two signals, not one fault. Vibration comes from the grinding bed and the hydraulic system that loads it: check the feeding first, then the hydraulic pressure and lubrication trends, then the bed geometry and the limit device. Rejects come from three different places — a protective reject gate that answers a feed-quality question, a classifier coarse return that answers a specification question, and a separator discharge that answers a moisture and separation question — and the fastest way to lose a day is to adjust the classifier instead of identifying which of the three has moved.
Record the six entries in section 10 and both investigations become comparisons rather than guesswork. The Vertical Roller Mill series carries five models covering 10-135 t/h with feed up to 38 mm, material-bed grinding that avoids metal-to-metal contact, hydraulic pressure compensation across the wear cycle, and an automatic reject function for ungrindable material; the closed-circuit classification side is covered by the RS Series Rotors Powder Separator, which holds 80-400 mesh with classification efficiency above 85% and returns coarse particles to the grinding chamber. Where the choice between this mill and a tube mill is still open, the machine-level comparison is set out in vertical roller mill or ball mill for cement and slag, and the wear and payback arithmetic sits alongside it in the analysis of vertical roller mill ROI in cement plants. Send your feed analysis, the material and the symptom you are seeing, and the cause can be traced against your own operating data rather than a general checklist.

About of Mascot
Zhengzhou Mascot Industry is a high-tech mining equipment company integrating R&D, manufacturing, sales, and after-sales service. Focusing on crushing, grinding, and mineral processing equipment, we provide professional solutions to our customers. We are ISO9001:2015 certified, and our products include mobile crushing plants, crawler crushing plant, construction waste crushing plants, jaw crushers, sand making machines, cone crushers, fine crushers, grinding mills, ball mills, etc., all with reliable performance to meet diverse project needs.
• Professional pre-sales support: Free project design and comprehensive solutions to help you accurately select the right equipment;
• Comprehensive on-site service: Providing installation guidance and worker training to ensure smooth equipment commissioning;
• Reliable after-sales guarantee: A complete after-sales system, timely response to technical inquiries and equipment maintenance, ensuring long-term stable operation.
To protect your rights, please contact us through the following official channels for professional service:
WhatsApp: 0086-16650273865
Email: mascot@mascotenv.com
We are committed to providing high-quality equipment and full-cycle services to deliver comprehensive intelligent solutions for the global mining industry!

The MTW series European grinding mill production line includes high-efficiency crushers, elevators, electromagnetic vibration feeders, milling machines, classifiers, and collectors. These pieces of equipment work together to achieve efficient crushing, grinding, and classification of various non-metallic ores, coal powder, slag, and other materials. It can meet the diverse needs of various industries for powder particle size, uniformity, shape, etc., and offer enterprises high-quality grinding products.

The Raymond mill production line is a highly efficient system designed for grinding operations, with a focus on energy efficiency, durability, and productivity. It caters to the needs of users by offering fine powder products in non-metallic ores, coal powder, and slag processing, aiding enterprises in achieving sustainable growth.

The high-pressure grinding mill production line is a project specially designed for efficient grinding operations. It is widely used in metallurgy, building materials, the chemical industry, highways, water conservancy hydropower, and other industries. It is a suspended roller mill that uses springs to increase pressure. It can achieve efficient grinding processing of various non-metallic raw materials. It has high efficiency, stability, and environmental protection characteristics.

The gypsum grinding production line is an efficient, stable, and environmentally friendly production solution, which is widely used in construction, decoration, the chemical industry, and other fields. In addition, the grinding process is particularly critical, which directly affects the quality and particle size of the final product. With the continuous development of science and technology, the technical level and production efficiency of gypsum grinding production lines will be further improved, providing strong support for the development of the gypsum processing industry.

This production line utilizes a three-ring medium-speed micro-grinding mill as the central equipment, complemented by other auxiliary equipment like hammer crushers, bucket elevators, and storage silos to establish a comprehensive grinding operation system. It has demonstrated strong potential for application and market competitiveness in industries such as construction, chemical industry, and new materials.
Green and Intelligent Mining Machinery
Manufacturing and Export Base
Based on high quality and perfect after-sales service, our products have been
exported to more than 120 countries and regions.
Copyright © 2023 Zhengzhou Mascot Environmental Technology Co., Ltd Record number: Yu ICP No. 13021523-4




 WhatsApp
